helen@hbxinnuorollforming.com
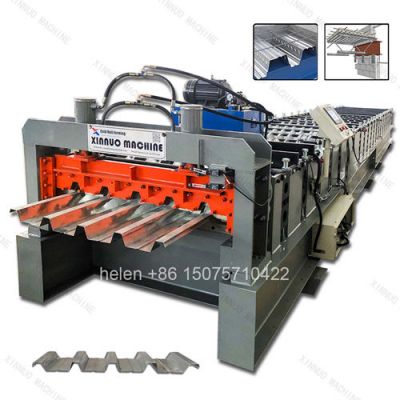
This Russia deck roll forming machine produces load-bearing Н-series profiled deck panels to the designation system used across Russia and the CIS. Instead of starting from a generic trapezoidal sheet, the roll set is cut for the exact working width, rib height and steel thickness your GOST designation calls for, so the finished panel matches what the structural design assumes.
Russian and CIS designers work from the ГОСТ 24045 profile range, where the type letter, rib height, working width and steel thickness are all part of the designation. The machine is set up for the specific designation in your specification.
| Profile | Rib height | Working width | Overall width | Steel thickness |
|---|---|---|---|---|
| H57-750 | 57 mm | 750 mm | Per drawing | 0.7 mm typical |
| H60-845 | 60 mm | 845 mm | 902 mm | 0.5-1.0 mm |
| H75-750 | 75 mm | 750 mm | 800 mm | 0.65-1.0 mm |
| H114 series | 114 mm | Per drawing | Per drawing | Per drawing |
| Deeper H grades | 150 mm and above | Per drawing | Per drawing | Per drawing |
Where the standard fixes the working width, the overall sheet width is wider because the outer ribs and the lapping edge sit outside the covered area. The feed strip width is set when the roll set is cut, so the forming train is designed around the coil width you can buy locally.
| Factor | What it means for the machine |
|---|---|
| Snow and wind loading | Deep Н-series ribs are specified far more often than in mild climates, so the forming train is longer and the frame heavier than for a shallow wall panel. |
| Standard designation | Working width and rib height are fixed by the designation, so the roll set must hit those dimensions, not a rounded local equivalent. |
| Steel thickness spread | 0.5-1.0 mm coil is common, so the frame and motors are sized for the top of the range you sell. |
| Zinc and polymer coating | Coated coil marks easily, so roll sets can be supplied with non-marking roll arrangements for pre-painted material. |
| Deck also used as permanent formwork | Panels often serve as non-removable formwork under a monolithic slab, so rib geometry and lapping edges matter as much as the covering width. |
The figures below are the proven configuration for the 750 mm Н-type profile, which has been supplied into Russia since 2014. Other rib heights are engineered to the same standard.
| Item | Specification |
|---|---|
| Profile type | ГОСТ 24045 load-bearing deck, type Н |
| Forming rows for 750 mm profile | 27 rows |
| Main frame | Heavy-duty 450H H-beam, 18 mm mid plate, shot blasted and painted |
| Shafts | 95 mm round bar, rough turned, cylindrical ground and chrome plated |
| Motors | 2 x 11 kW, dual drive |
| Transmission | 2-inch chain drive |
| Feed strip width | 1250 mm for a 750 mm working width |
| Forming rollers | Forged 45# steel, quench hardened, polished and chrome plated |
| Cutting | Hydraulic shear, cut to length, square panel ends |
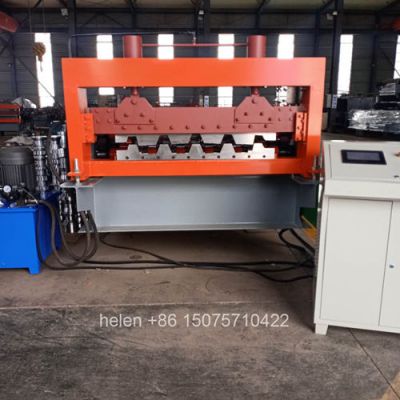
| Control | PLC with touch screen, length and quantity setting |
| Power supply | 380 V or 415 V, 3 phase, 50 Hz, built to site requirement |
| Line length | About 22 m including decoiler, control cabinet and output table |
| Section | Function |
|---|---|
| Decoiler | Carries the coil and feeds strip under steady tension |
| Feed guide | Aligns the strip to the forming centreline |
| Main forming unit | The longest section of the line, because deep ribs need many passes |
| Shear | Cuts the deck panel to the ordered length |
| Output table | Receives finished panels for inspection and bundling |
| Control cabinet | Length, quantity and speed setting with panel counter |
Allow about 25 m of length and 5-6 m of width for a deep-rib deck line, with enough height for coil handling by crane.
| Item | Note |
|---|---|
| Material | Galvanized or pre-painted steel coil to the grade named in your specification |
| Thickness | Tell us the full range you intend to sell; the frame is sized for the top of that range |
| Coil inner diameter | Matched to the decoiler mandrel at order stage |
| Coil weight | Stated on the order so the decoiler is sized correctly |
| Surface | Non-marking roll arrangement available for polymer-coated coil |
| Question | Answer |
|---|---|
| Can you work from a GOST designation instead of a drawing? | Yes. Send the designation and we confirm the resulting working width, rib height and feed width in writing before the roll set is cut. |
| What strip width do I need for a 750 mm profile? | On the proven 27-row configuration we run a 1250 mm feed for a 750 mm working width. The exact figure is confirmed for your profile. |
| Will the line run 0.5 mm and 1.0 mm coil on the same roll set? | It will, within the range agreed at order stage. The frame, shafts and motors are sized for the thickest material, and the roll gap is set for each coil. |
| Can the line also run a shallow wall or roof profile? | Forming rolls are cut for one profile family. If you also need a shallow sheet, we quote a second roll set or a separate machine, depending on your volume. |
| Will the panel match the declared working width? | Yes. The roll set is cut to the declared working width, and the sample panel from the trial run is measured and recorded before shipment. |
Hebei Xinnuo is a professional cold roll forming machinery manufacturer with 20+ years of experience. We specialize in C/Z purlin machines, roof panel roll formers, floor deck machines, and custom profile solutions — exported to 50+ countries worldwide.